Boiler Chemical Manufacturers in Pune | Chemion Speciality Pvt Ltd
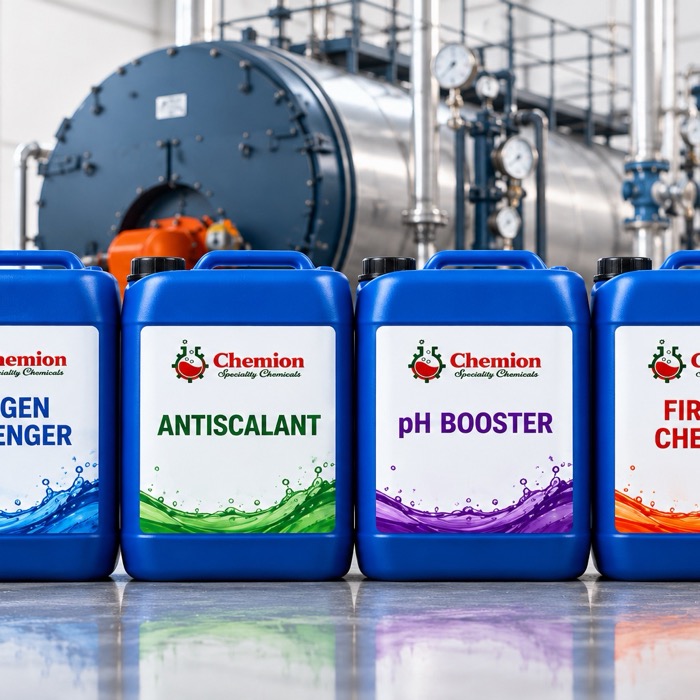
Chemion Speciality Pvt Ltd is leading Boiler Chemical Manufacturers, Suppliers, Dealers, and Traders in Pune. Boiler chemicals play an important role in maintaining the efficiency, reliability, and operational performance of industrial boiler systems. Proper water treatment helps control scale formation, minimize corrosion, and manage impurities that can affect heat transfer and equipment life.
Industrial boilers operate under different pressure and temperature conditions, making effective water chemistry management essential for consistent steam generation. Selecting suitable chemical treatments helps reduce deposit-related problems and supports reliable plant operations.
We provide boiler chemical solutions designed to address water quality challenges across various industries. Our focus is on supporting scale prevention, corrosion control, deposit management, and efficient boiler operation through suitable chemical treatment programs.
What Are Boiler Chemicals?
Boiler chemicals are specialized formulations used to manage water chemistry in boilers and associated steam systems. Depending on their composition, they help control hardness, dissolved oxygen, pH, sludge, and other factors that may contribute to scale formation or corrosion.
Boiler Water Treatment Process
- Feedwater Analysis: The process begins with evaluating feedwater quality, including hardness, pH, alkalinity, dissolved oxygen, and other relevant parameters. The results help determine the required treatment approach.
- Chemical Selection and Dosing: Suitable products are selected according to boiler design, operating pressure, water quality, and treatment objectives. Chemical dosing must follow technical recommendations and appropriate safety procedures.
- Water Chemistry Monitoring: Regular testing helps verify that key parameters remain within the recommended operating ranges. Monitoring allows adjustments when feedwater quality or operating conditions change.
- Blowdown and Deposit Management: Controlled blowdown removes accumulated dissolved and suspended solids from the boiler. This process helps maintain water quality and supports effective chemical treatment.
Types of Boiler Chemicals
As we are leading Boiler Chemical Manufacturers in Pune, Our Types are designed to meet different application requirements and industry standards, including the following types:
- Boiler Antiscalant Chemicals: These formulations help inhibit mineral crystal formation and reduce scale deposits on heat-transfer surfaces. Their effectiveness depends on water composition and operating conditions.
- Boiler Scale Inhibitor Chemicals: These chemicals help control hardness-related deposits inside boiler tubes and other components, supporting heat-transfer performance and reducing maintenance requirements.
- Boiler Corrosion Inhibitor Chemicals: Corrosion inhibitors help reduce metal deterioration by controlling corrosive conditions and supporting the protection of compatible boiler surfaces.
- Boiler Oxygen Scavenger Chemicals: These treatments react with dissolved oxygen to reduce oxygen-related corrosion. The selected product must be compatible with the boiler's operating conditions.
- Boiler Descaling Chemicals: Descaling products help dissolve or loosen existing mineral deposits during controlled cleaning procedures. Selection depends on deposit composition and equipment materials.
- Boiler Cleaning Chemicals: These formulations are used to remove selected contaminants, residues, and deposits during planned boiler cleaning and maintenance activities.
- Boiler Phosphate Treatment Chemicals: Phosphate-based treatments help control calcium hardness through precipitation and conditioning when appropriate for the boiler water treatment program.
- Boiler Sludge Conditioner Chemicals: These products condition suspended precipitates and sludge, helping keep deposits manageable and supporting removal through suitable blowdown practices.
- Boiler Anti-Foaming Chemicals: Antifoaming agents help reduce excessive foam formation in boiler water, lowering the risk of water carryover and supporting steam quality.
- Boiler Passivation Chemicals: Passivation treatments help establish or stabilize protective oxide layers on compatible metal surfaces during controlled commissioning, maintenance, or treatment procedures.
Boiler Water Treatment Solutions
As a trusted Boiler Chemical Suppliers in Pune, we serve businesses across various industries that meet professional visual communication requirements.
| Treatment Solution | Primary Function | Key Benefit |
|---|---|---|
| Scale Prevention | Controls mineral deposits on heat-transfer surfaces | Helps maintain heating efficiency |
| Corrosion Control | Manages corrosive conditions in boiler water | Protects compatible metal components |
| Oxygen Removal | Reduces dissolved oxygen through suitable treatment | Minimizes oxygen-related corrosion |
| pH and Alkalinity Control | Maintains appropriate water chemistry | Supports boiler system protection |
| Sludge Conditioning | Helps manage suspended precipitates and deposits | Supports effective blowdown |
| Condensate Treatment | Helps control corrosion in condensate return lines | Protects condensate system components |
| Deposit Removal | Dissolves or loosens compatible existing deposits | Supports planned cleaning and maintenance |
| Foam Control | Reduces excessive foam formation | Helps minimize water carryover into steam |
Features and Benefits of Boiler Chemicals
As Boiler Chemical Dealers in Pune, our products provide several Features and Benefits including consistent quality, smooth finish, and long service life.
| Feature | Description | Benefit |
|---|---|---|
| Scale Prevention | Helps control mineral deposit formation | Supports heat-transfer efficiency |
| Corrosion Control | Helps manage corrosive water conditions | Reduces metal deterioration |
| Oxygen Management | Reduces dissolved oxygen where applicable | Helps protect boiler components |
| pH Regulation | Maintains suitable water chemistry | Supports system reliability |
| Deposit Conditioning | Helps manage selected suspended solids | Supports effective blowdown and maintenance |
Applications of Boiler Chemicals
As Boiler Chemical Traders in Pune, our all types are used in various types of industrial sectors such as:
- Manufacturing Industries: Boiler treatment supports steam generation for process heating, production equipment, and other industrial operations.
- Food and Beverage Processing: Suitable treatment programs help maintain boiler performance in facilities using steam for processing, heating, and cleaning.
- Pharmaceutical Plants: Appropriate water treatment supports utility boiler operation, subject to applicable process requirements and water quality controls.
- Textile Industries: Boilers supply steam for dyeing, finishing, and other textile processes that require consistent heat.
- Chemical Processing Plants: Treatment programs help manage boiler water chemistry in facilities that depend on steam for industrial processing and heating.
- Paper and Pulp Industries: Boiler chemicals support steam-generation systems used in pulp processing, drying, and other manufacturing operations.
- Power Generation: Suitable chemical treatment helps manage water chemistry in steam-generation equipment and supports reliable plant operation.
- Hospitals and Healthcare Facilities: Boilers provide steam and hot water for selected utility applications, with treatment requirements determined by the system and intended use.
- Hotels and Commercial Buildings: Water treatment helps maintain boilers used for heating, laundry, hot water, and other building services.
- Sugar and Distillery Plants: Boiler treatment supports steam generation for process heating, evaporation, and associated industrial operations.
Why Choose Us?
As one of the leading Boiler Chemical Manufacturers in Pune, we deliver premium-quality solutions designed to meet diverse industrial requirements. Here's why we stand out:
- Application-Based Solutions: We focus on matching chemical treatment options to boiler design, feedwater quality, and operating conditions.
- Quality-Focused Products: Product selection and handling follow applicable specifications and documented quality requirements.
- Technical Guidance: We help identify relevant treatment considerations based on water analysis, system conditions, and maintenance objectives.
- Customized Treatment Programs: Treatment recommendations can be tailored to the requirements of compatible boiler systems and their operating environments.
- Customer Support: We aim to assist customers with product information, application guidance, and the selection of suitable treatment solutions.
Choose Chemion Speciality Pvt Ltd is leading Boiler Chemical Manufacturers, Suppliers, Dealers, and Traders in Pune. Effective boiler water treatment is essential for managing scale, minimizing corrosion risks, maintaining heat-transfer performance, and supporting reliable industrial operations. Choosing suitable chemicals requires careful consideration of water quality, boiler design, and operating conditions.
Our boiler chemical solutions are designed to support appropriate water conditioning across a wide range of industrial applications. Contact our team today to discuss your boiler treatment requirements and request product recommendations or a quotation.
FAQ’s
They help control scale, corrosion, dissolved oxygen, and other water chemistry problems that can affect boiler efficiency and reliability.
Selection depends on feedwater analysis, boiler pressure, operating conditions, and the existing treatment program. Consult a qualified water treatment specialist.
Testing frequency depends on boiler design, operating conditions, and the treatment plan. Regular monitoring helps identify water quality changes before they affect performance.
Certain descaling formulations can remove compatible deposits through controlled cleaning procedures. The process must account for deposit composition, equipment materials, and safety requirements.
No. Compatibility varies by formulation, water chemistry, pressure, temperature, and system materials. Follow manufacturer instructions and qualified technical guidance.